

Why consistency matters in autoclave-free lamination
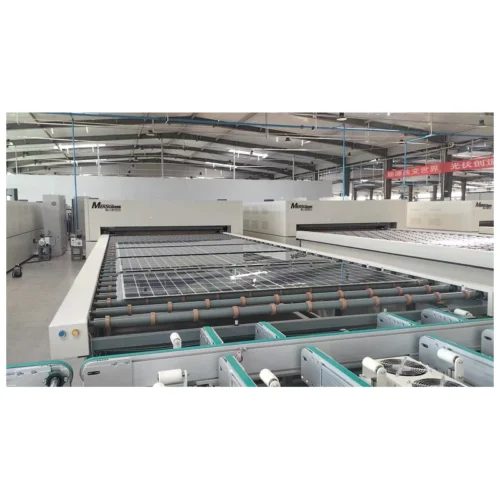
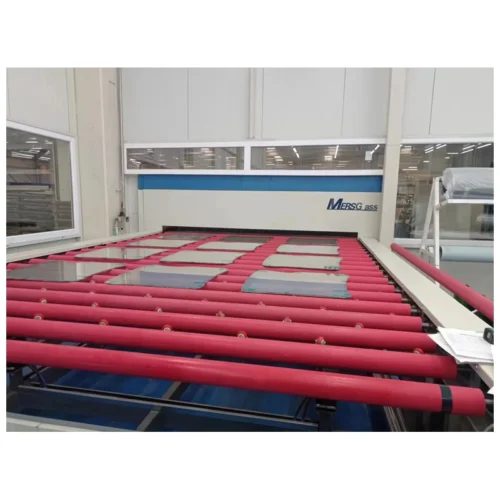
In a non-autoclave laminating line, the glass stack is bonded in a continuous flow rather than in a high-pressure autoclave batch. That makes process control the deciding factor: every sheet must see the same temperature curve, the same pressing force and the same cooling rate.
Three control points on the line
- Heating zones: independently controlled zones bring the glass and interlayer up to bonding temperature gradually, reducing thermal stress and edge defects.
- Pressing section: stable pressure across the working width helps the PVB, EVA or SGP interlayer bond evenly without trapped air.
- Cooling and unloading: controlled cooling before the unloading table keeps the laminate flat and ready for the next process step.
What to check before accepting a line
Ask for a trial run with your own glass sizes and interlayer film, and review the recorded temperature and pressure curves. A line that can repeat the same recipe shift after shift is more valuable than one that only reaches a high peak output.
Contact our engineers for a line layout and a specification sheet for your plant.